Best-in-Class Packaging machine | Clearpack
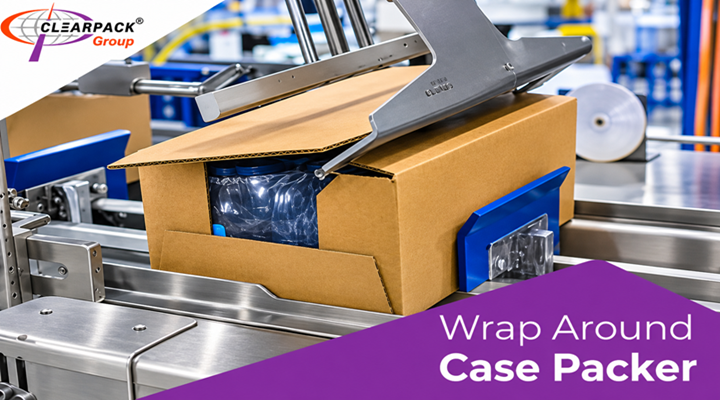
RSC (Regular Slotted Container), also known as American-style cases, are a popular choice for packaging because they can be manually erected or handled using various automated case-packing solutions. However, operational managers who continuously seek ways to reduce overall packaging costs are increasingly considering wrap-around case packing as a cost-effective and sustainable alternative.
Let us discuss its advantages:
What is Wrap Around Case Packing?
In wrap around case packing, the carton blanks are loaded and wrapped around the product to be packed to form a compact and robust box, sealed with hot glue.
It's Advantages
1. Saves Packaging Material: Since the corrugated blank is designed to fit the dimensions of the product, material wastage is minimized. This can result in significant savings in corrugated board costs, particularly when packaging products in cases with lower heights. Furthermore, when working with a corrugated case supplier, the need for a separate pre-gluing process for the manufacturer's joint (also known as the industrial flap) is eliminated, as the joint is glued and sealed directly on the wrap-around case packer. This eliminates an additional processing step at the supplier's end. Moreover, the compact design of wrap-around cases allows more cases to be transported on the same pallet, helping reduce logistics costs and the overall carbon footprint.
2. Saves Time: Wrap-around case packing allows more corrugated blanks to be stored in the magazine compared to conventional RSC case blanks. As a result, the operator needs to replenish the magazine less frequently, reducing machine downtime and manual intervention. This allows the operator to spend more time on other productive activities, improving overall operational efficiency.
3. Improved Case Strength: The tight folding and sealing of the corrugated board around the product create a firm and structurally stable case, providing better product protection and package integrity. The improved case design can also enhance stacking strength, potentially allowing for better pallet optimization by increasing the number of cases stacked vertically without compromising load stability.
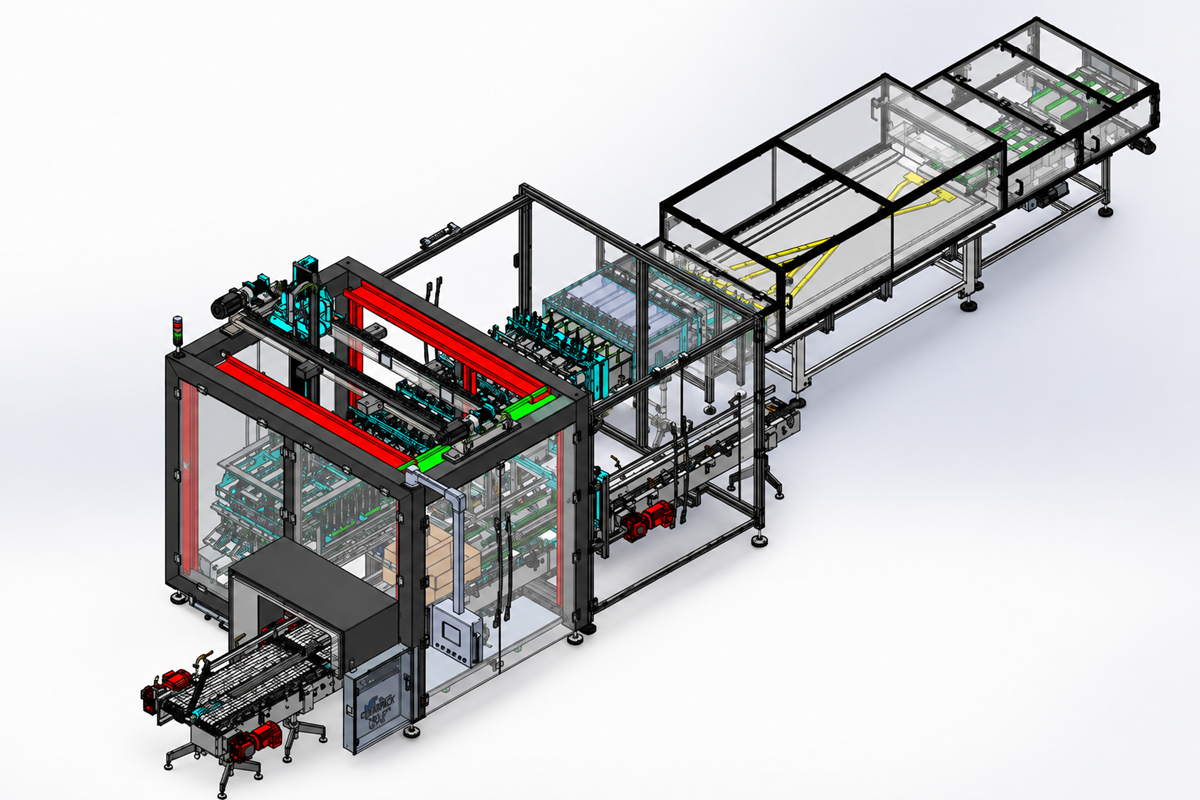
4. Saves Floor Space: Case forming, product loading, and sealing are carried out in a single compact wrap-around case packing machine, reducing the need for valuable factory floor space compared to conventional RSC lines that may require three separate machines: a case erector, case packer, and case sealer.
5. Multiple Formats: Wrap-around case packing machines can handle corrugated and solid board blanks to produce full-size wrap-around cases, trays, and Shelf-Ready Packaging (SRP). Depending on the machine configuration, both wrap-around cases and trays can be produced on the same machine with minimal adjustments.
6. Suitable for FMCG, Lubricants, and Pharmaceutical Industries: Wrap-around case packing offers the flexibility to handle a wide variety of products, multiple packaging formats, and diverse production requirements across these industries.
7. Sustainable Packaging: The use of recyclable corrugated materials, efficient material consumption, and reduced packaging waste makes wrap-around case packing a more environmentally sustainable packaging solution.
For more information, visit www.clearpack.com or write to us at info@clearpack.com.
...